This page introduces the main components of the X-Smart 5 3D printer, aiming to provide you with a comprehensive understanding of the printer.
¶ How does X-Smart5 work?
The X-Smart5 3D printer is a machine that uses plastic filaments to create three-dimensional objects.
In most cases, the X-Smart5 can read and print 3D Gcode/3mf format files, so it requires preprocessing of the file model(STL, OBJ, 3MF,STEP,STP, etc.) using slicing software before printing.
Taking QIDI Studio as an example, the slicing software divides the STL file into many layers and automatically converts the information of each layer into a language that the printer can understand, indicating the motion paths and speeds of each axis during the printing process.
In addition, slicing software can integrate various parameter settings in the generated code, such as the printing temperature of the filament and the extrusion speed of the printer, and generate support structures for certain parts of the printed model.
¶ CoreXY Motion System
The QIDI X-Smart5 utilizes a CoreXY motion system controlled by two stepper motors. The stepper motors on the X-axis and Y-axis work together to move the print head.
Each stepper motor is connected to the print head via an independent belt, thus a pair of belts are used to control its position. The adoption of the CoreXY motion system enables the X-Smart5 to print at a faster speed compared to traditional Cartesian printers, as its moving parts are lighter in weight, which is particularly important for high-speed printing.
For more information about the CoreXY motion system, please refer to this link.
¶ Z-axis
The Z-axis consists of four lead screws, which are connected to a single stepper motor via a belt.
¶ Tool Head(Print Head)
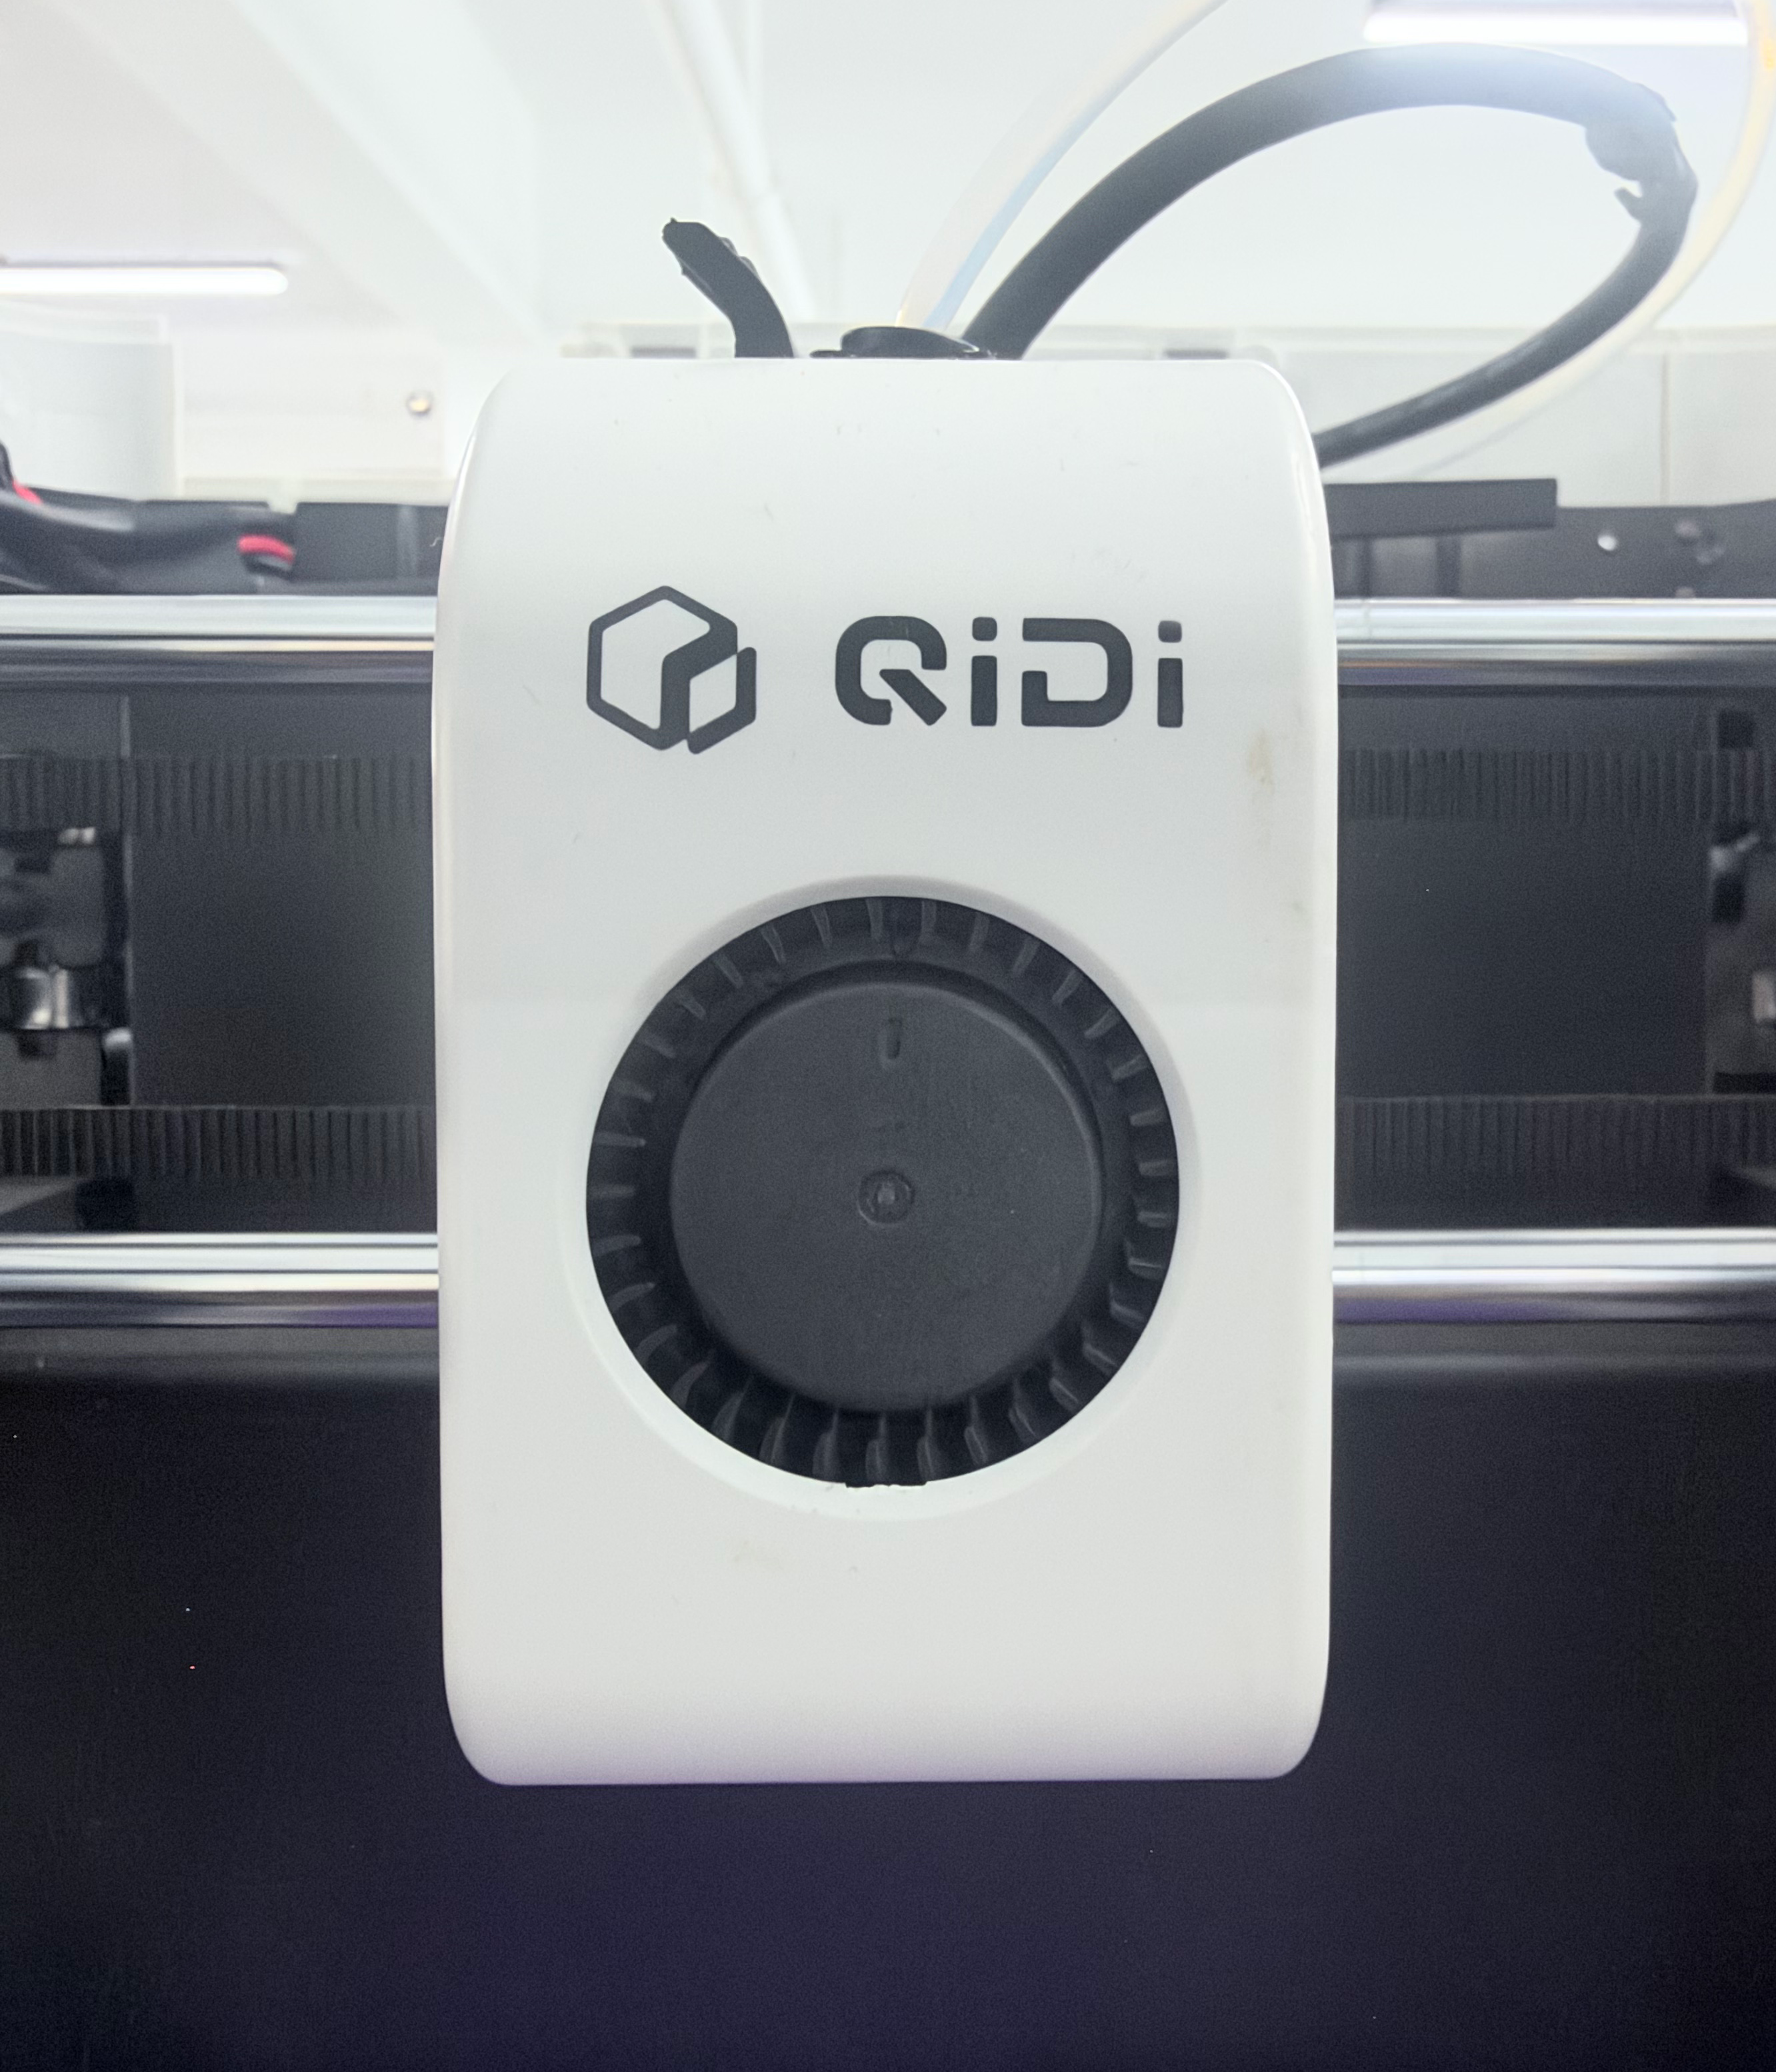
¶ Extruder
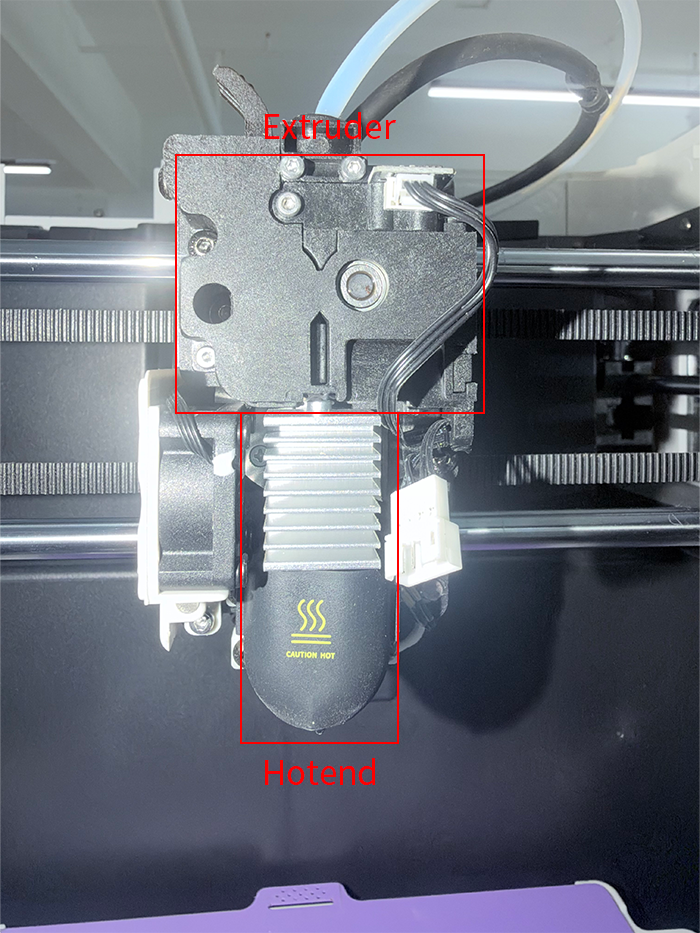
The extruder is responsible for pulling out the filament from the spool and feeding it into the hot end. After being heated and melted, the filament is extruded through the nozzle to generate the printed model. The extruder requires precise control over the length of the filament extruded through the hot end and is one of the core components of a 3D printer.
¶ Hot end
The hot end is responsible for heating the filament to a specified temperature, causing it to melt and deposit in thin layers to create the model. Different materials require different heating temperatures. For example, PLA filament needs to be printed at a lower temperature of around 210-220°C, while other materials such as PETG and ABS require higher temperatures of around 250-260°C for printing.
¶ Hotbed
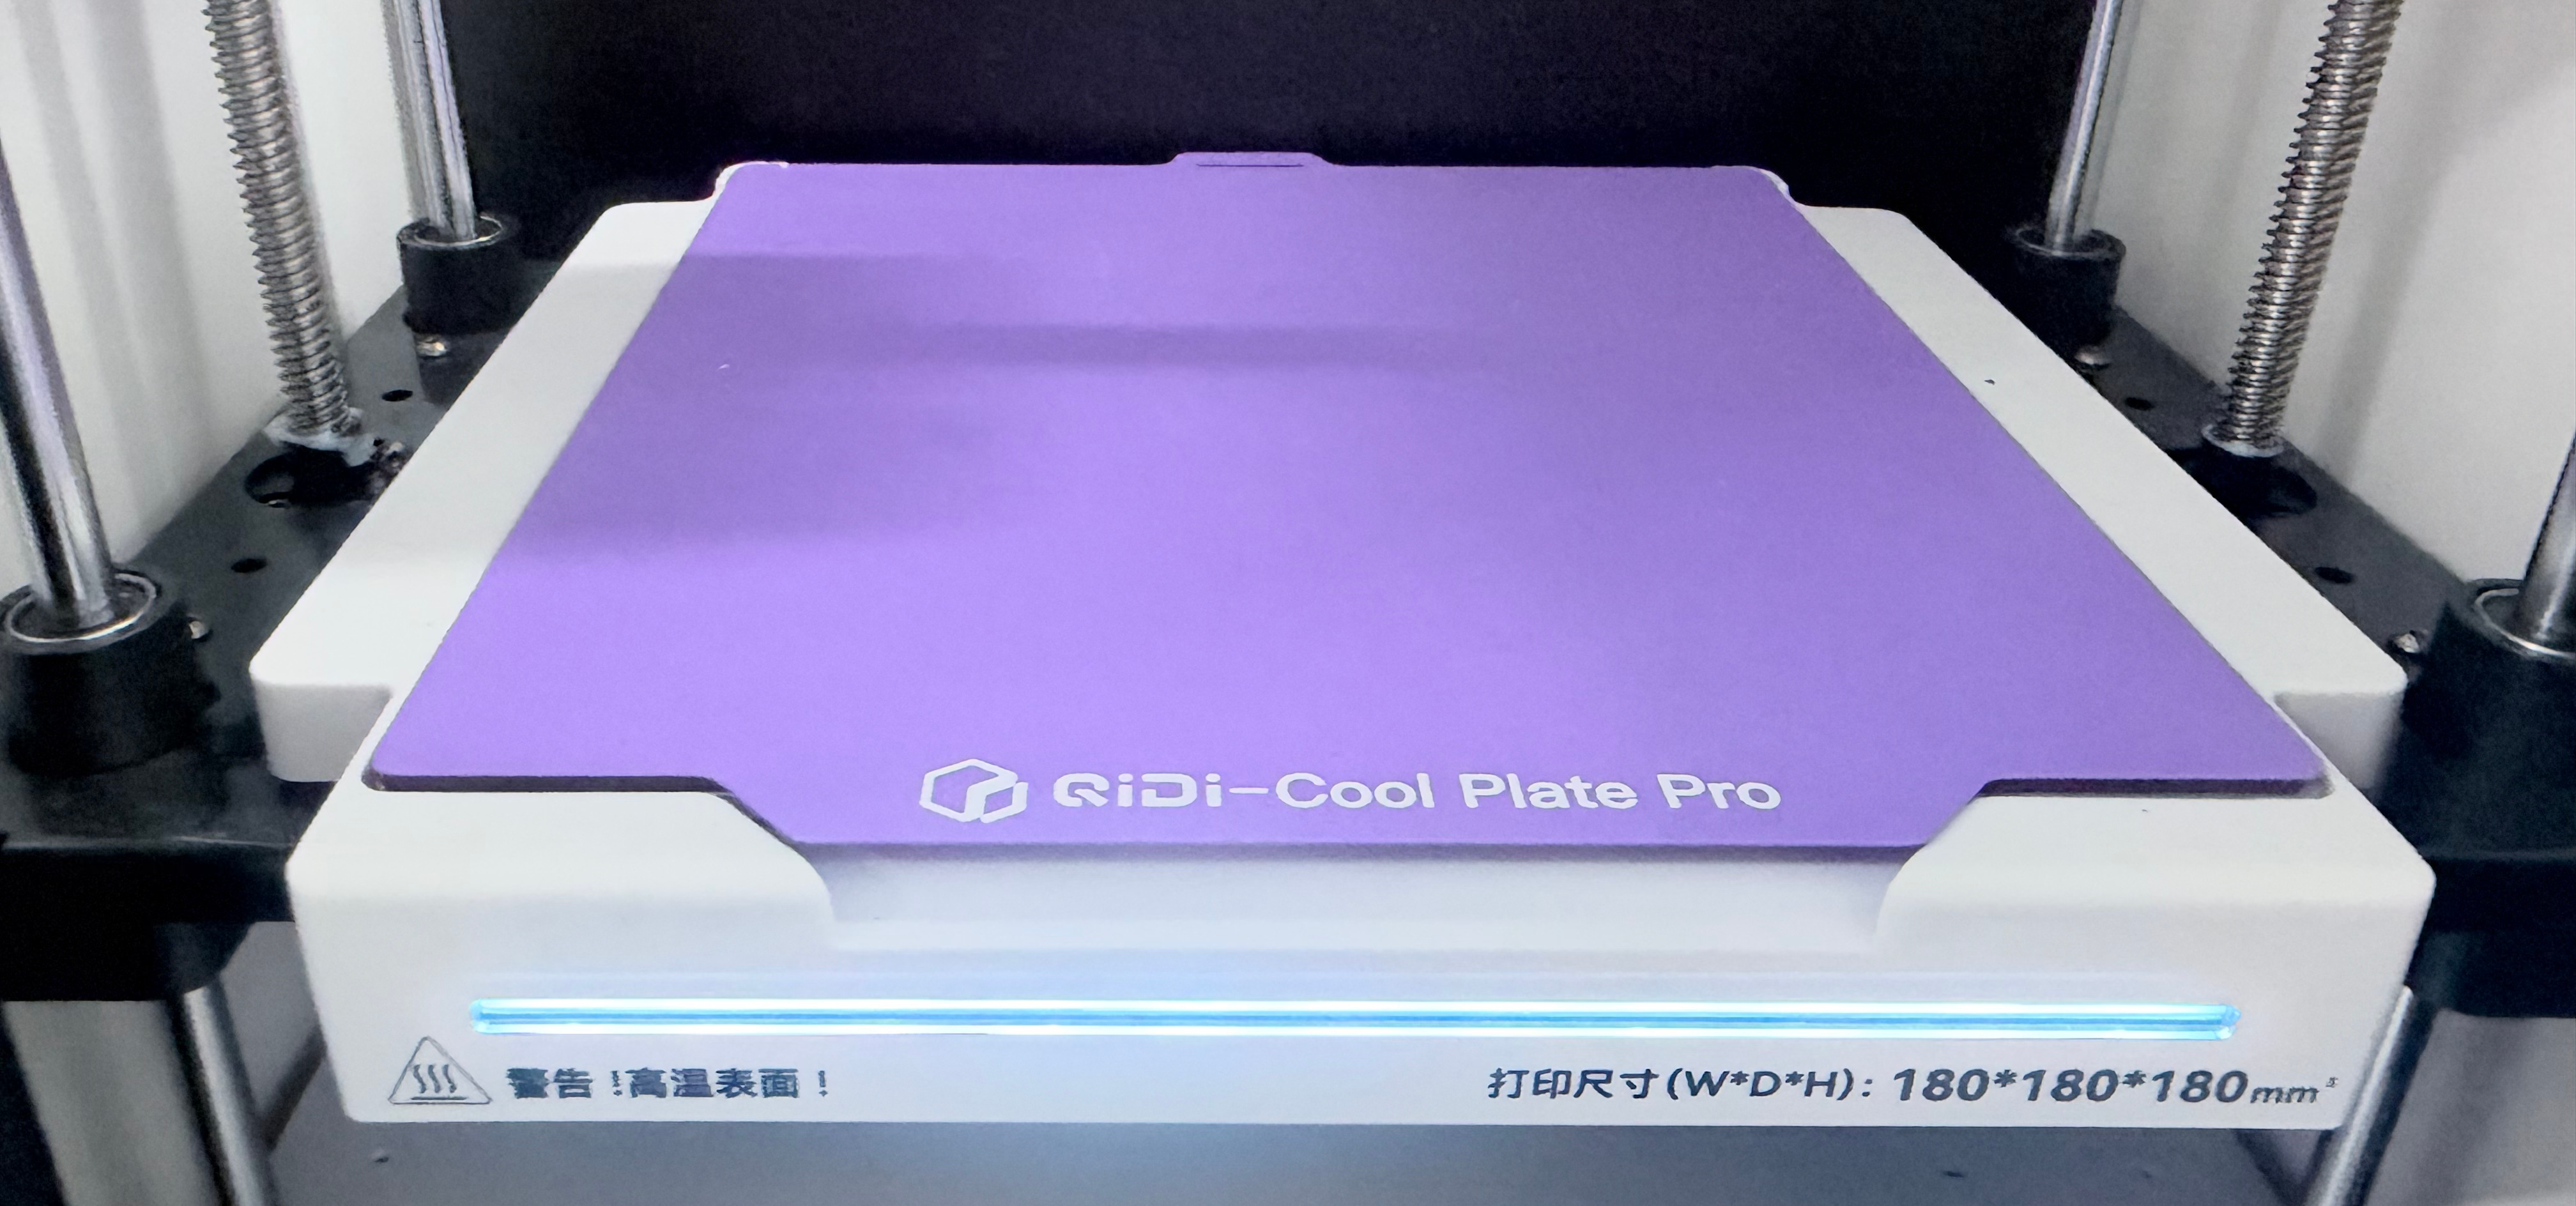
The heated bed warms the printing surface to help printed layers adhere better to the build plate.
When using the X-Smart5 3D printer, adjust the heating temperature according to the filament type; the maximum temperature is 80°C. For example, PLA can be printed on the low-temperature build plate at a bed temperature of 35–45°C without warping.
¶ Breathing light
Display the current printing status